Parison Stability in BM1052 Drum Blow Molding
2026-10-14 · Ascent Group Editorial
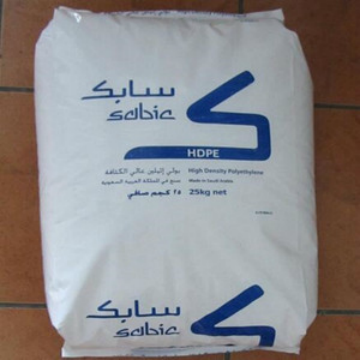
Wall thickness uniformity on a 200 L drum starts in the die, not the mold. BM1052 pairs a broad molecular weight distribution with a 0.05 g/10min low-shear flow, so the parison hangs straight during the long drop a drum tool needs.
Converters tune three levers: die gap and land length for melt orientation, pre-blow timing to set the parison before inflation, and parison programming to add material at the base chime where stress concentrates. Because BM1052 resists sag, the programmed profile survives from head to clamp without thinning.
The payoff shows in testing: drums blow from a stable parison pass drop and stacking loads with less regrind, and wall readings at the base and chime stay close to target across shifts.